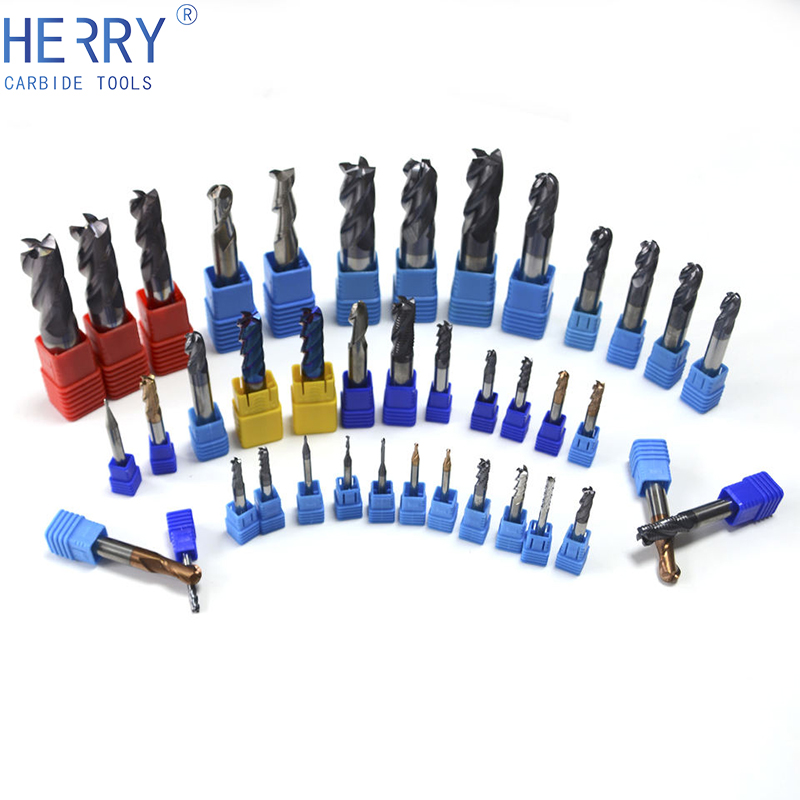
All About End Milling - end mill flat
A carbide Jobber Length Drill is the standard general-purpose drill within Titan USA’s offering. It has a long flute length and an included angle of 118o. These drills are great for general purpose drilling where the tolerances are not as tight as the Stub Drill or Straight Flute Drill. Due to the length of these drills, however, they will be more affected by any lack of rigidity in the set up and can have higher runout, or straying from a desired location, during the drilling operation.
When navigating Titan USA’s offering of carbide drills, it is imperative to understand the key differences among the three carbide drill styles: Jobber Length, Stub Length, and Straight Flute Drills. The right drill for your application depends on, among other factors, the material you are working in, the job requirements, and the required accuracy.
All machine tool operations consist of a cutting tool (e.g., a drill bit) and the workpiece that is being machined to make something. So, if you're drilling a hole in a piece of wood, then the wood is the workpiece.
MechanicsLengthDrill bits
Titan USA carbide Stub Length Drills have a shorter flute length, wider included point angle, and a significant drop in helix angle, when compared to Jobber Length Drills. The shorter length and wider tip create for a more rigid tool and, in turn, more accurate holes. The stub drill is the best option when drilling with tight tolerances on shallower holes.
Drill bitlengthChart
Carbide drills are ideal for high-volume hole production. They are perfect for CNC machining and help to get the desired accuracy. You need to select the right carbide drill according to your operation. The article provides complete information on the titan carbide drills. Thanks for the insights. I will be sharing it with my friends.
So it's a reamer speed and feeds, milling speeds and feeds, and drill feeds and speeds calculator (plus more) all rolled into one.
Helix drills create multiple different forces on the part, which can create micro imperfections. The Straight Flute Drills do not create those forces, so the finish is much more consistent down to the micro level. The margins of the Straight Flute Drill also burnish the inside of the hole as they spin, which improves the finish as well. When comparing the Straight Flute Drill to a helix drill, the length of the overall contact point is much shorter in the Straight Flute Drill, and has less heat generation. The decreased heat will also reduce the probability of work hardening.
Finally, it supports the turning operation where the cutting tool is stationary, and the workpiece rotates. This configuration is the essential operation of a lathe machine, which is used to create symmetric circular manufactured items.
Selecting the correct carbide drill for your application is a crucial step in hole making. The Jobber Drill is a great general-purpose drill and should be utilized in applications requiring long reach. The Stub Drill increases the rigidity with its shorter length of flute, allowing it to drill with higher accuracy. Applications which involve tight tolerances and more shallow holes can be done with the Stub Drill for high-quality results. Lastly, for difficult to machine and hard materials, the Straight Flute Drill is the perfect solution. When the core diameter and chip evacuation is properly addressed, the Straight Flute Drill produces beautifully consistent surface finish and extremely tight tolerances. Similarly, Titan USA offers its carbide drills in both an uncoated option, and AlTiN coating. Traditionally, uncoated tools are general purpose workhorses in a wide variety of materials both ferrous and non-ferrous. AlTiN or Aluminum Titanium Nitride is an enhanced coating specifically made for ferrous materials that extends tool life and performance across a wide range of steels and their alloys.
What isajobberdrill bit used for
With the calculator mode set to manual mode, you need to enter the minimum and maximum surface speeds and chip loads. The specification sheet for the tool you are using may contain this data. Here's what you should do:
If you are using the metric system and have the surface speed VVV in meters per second and the diameter DDD in millimeters, the equation is:
Carbide Straight Flute Drills have the smallest core of the three drill types mentioned within this post. Titan USA offers Straight Flute Drills with 2 flutes and a 140o included angle. These drills are designed for hole making in materials that create short chips. Materials in which the Straight Flute Drill typically performs best include cast aluminums and cast irons, as well as copper. In addition, this type of drill can work very well in high hardness materials, but the core diameter should first be adjusted to accommodate the increased hardness. For these difficult to machine materials, casting the part with a core hole and then opening it up with the Straight Flute is a great option. This removes some of the stress caused by chip removal and allows for the drill to do what it does best.
In manual mode, you can set the cutting speed (usually in surface feet per minute – sfm), and it will output the rotation speed in rotations per minute (rpm), therefore converting sfm to rpm. You can also set custom chip loads to calculate the feed rates. Let's look at each mode in detail next.
Jobber lengthmeaning
Next, enter the number of teeth the tool has to get the range of feed rates to use. The feed rates shown are for the average rotation speed. To calculate the feed rates at a different speed, enter the RPM into the custom rotation speed field. Similar to rotation speed, the slower the feed rate, the smoother the finish of the operation will be.
The "speeds" part of the speeds and feeds calculator is the rotation speed of either the tool (e.g., for drilling) or the workpiece (e.g., for turning on a lathe). For a given tool and workpiece material, there is a range of recommended cutting or surface speeds between the two materials. Given the surface speed, you can calculate the spindle speed in revolutions per minute (RPM) using the following equation (when using imperial units):
Jobberdrill bitlength
To achieve high accuracy and great finish, consider utilizing a Reamer. Reamers are designed to remove a finite amount of material but bring a hole to a very specific size. To do this, first drill 90% – 94% of the desired hole diameter with a Jobber Drill. After 90% – 94% of the material is removed, go in for a finishing pass with a Reamer. Reaming tools are highly accurate and leave a beautiful finish.
Continue reading to learn about machine tool operations and the two principal speeds and feeds formulas that power this calculator.
Chip evacuation can be an obstacle for hole making. Pecking cycles can be used to aid in chip removal. Peck cycles are when the drill is brought in and out of the hole location, increasing depth each time until the desired depth is reached. However, pecking cycles should only be used when necessary; this process increases cycle time and subjects the tool to added wear from the repeated engaging and disengaging.
Sign up to receive a monthly recap of: – The latest machining solutions – Machining tips and tricks – A recap of our most popular posts
Jobberdrill bit size chart
Jobber lengthvs mechanicslength
The calculator will produce a recommended range of feed rates. Generally, it would be best if you started at the lower feed rate and slowly increase it from there. For an operation such as milling, the slower the feed rate (and cutting speed), the smoother the finish on the workpiece will be.
You will then see results for the range of speeds you should use. For the best outcome, start at the minimum speed and gradually increase it to the average figure. If you want a quick, but rough finish, carry on up to the maximum speed.
Omni's speeds and feeds calculator helps you set the correct rotation speed and feed rate of your machine tool. It supports all of the following machine tool operations:
If you are not sure how many teeth your tool has, look at it end-on and count how many sharp cutting edges there are around the circumference of the tool.
Drill bit lengths explained
In preset mode, you can select the operation, tool material, size and number of teeth, and the workpiece material. The calculator contains a range of recommended cutting speeds for different materials, allowing it to calculate the rotation speeds. It also has the corresponding chip load data to calculate the feed rates.
Analyzing the equation, you might notice that π×D\pi \times Dπ×D is the formula for circumference of a circle. So we're dividing the speed at the circumference by the distance traveled during one rotation to get the number of rotations per minute.
Chip removal can be more difficult in this style of carbide drill because the chips are not guided along a helix. With helix flutes, the motion of chip removal is mostly continuous from their initiation point, through the flute valleys, and finally out of the flute valleys. The helix creates a wedge which helps push the chips along, but the straight flute does not have that. It interrupts that natural turning motion created by the drill face which can affect chip evacuation. Due to the interruption in motion this type of drill is better suited for applications involving chips of smaller size.
Let's go through an example of how to calculate speeds and feeds manually, using the speeds and feeds formulas discussed above. Your tool is half an inch in diameter and made of high-speed steel, and you are end-milling a block of aluminum. Looking up the average surface speed between the cutting tool and the aluminum, you find it to be 600 feet/min. Using the imperial speeds formula, you would perform the calculation:
Are you planning a general home renovation? Go ahead and check our stair calculator and the decking calculator – they may come in handy!
The chip load depends on the characteristics of the tool and the workpiece material. For example, a tool drilling a hole into a soft workpiece material will have a higher chip load than a harder workpiece material.
Next, let's calculate the average feed rate at 4584 RPM4584\ \mathrm{RPM}4584 RPM, given that your tool has two teeth, and it has an average chip load when milling aluminum, which is 0.0040.0040.004 inches:
Ideally, you would also calculate the minimum and maximum speeds and feeds, so let's see how our calculator can work out everything for you in super-quick time.
The term "feeds" refers to the feed rate or the relative linear speed between the tool and the workpiece. For example, for drilling, it is the speed at which the drill bit travels down into the workpiece material. The equation for the feed rate is:
www.harveytool.com www.helicaltool.com www.micro100.com www.titancuttingtools.com www.corehog.com www.valorholemaking.com
 18581906093