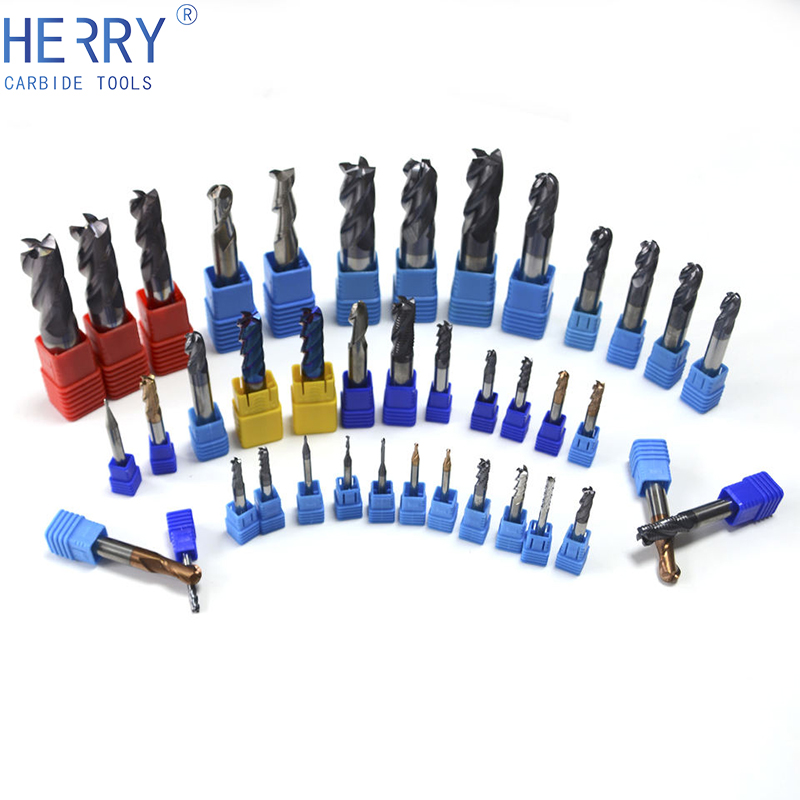
All About End Milling - endmil
“While the small stepover would slow the hogging removal rate a little,” said DeLucca, “the resulting scalloped peaks would be small enough to meet tolerances without subsequent operations and attendant tool changes.” At 0.060-in. stepover, a 0.75-in. cutter leaves scallop ridges just 0.002-in. high, well within tolerances for the part.
Ingersoll DHU plunge cutter delivers pure axial cutting forces for faster machining with no lateral forces that can cause tool failure or uneven results due to tool deflection.When end milling long pockets, cutting forces can cause deflections along the tool’s X and Y axes resulting in workpiece dimensional variations. These forces can lead to tool breakage. On the other hand, with plunge milling, the cutting force vector runs straight up the tool centerline, so you can cut with more force without fear of bending or snapping the tool. Plunge milling works much like drilling: plunge straight in, withdraw, step over plunge again, and so on. Since all the cutting force vectors are right up the tool’s strong centerline, you can safely feed faster by plunging along the Z axis than by end-milling along the X and Y axes. Plunging leaves a scalloped wall that may require finish milling, depending on tolerances and size of the stepover. Plunge cutters also have built-in chip evacuation capacity, so blast air or liquid coolant is helpful but not required on vertical setups. Associated Technologies and Manufacturing Inc., a 25-man Baton Rouge contract fabrication shop specializing in silicon and energy oil country components, found plunge milling to be the answer to its production problems. ATM wished to speed up production and cut high tooling costs when endmilling long pockets in a steel prone to work hardening. The company switched from a solid cobalt end mill to a two-flute Punch- In Quad DHU Series indexable plunge mill from Ingersoll Cutting Tools. “With that one simple processing change, we’ve made work hardening a thing of the past, saving us 10 hours of machining time and $880 in tooling per part,” said Glen Kollars, lead machinist at ATM. “Now we complete a 44-in.-long square-sided pocket with a single tool instead of three. The plunge mill paid for itself on the very first part.” Eliminating deflection The part is an 8.375-in.-diameter by 100-in.- long shaft of wrought 4140 HT steel with two opposing pockets running lengthwise. The pockets will contain instrumentation that must fit within the shaft diameter. Measuring 44-in. long with a 4.750 by 3.625-in. cross section, the pockets have straight sides, flat bottoms and reliefs in the corners to accommodate a tightfitting sharp-cornered cover. After machining, a 1.125-in. web separates the two pockets.
... Thread Mills · Custom PCD / CBN Milling Tools ... JBO Shark Thread Mill Video Demo. Test Specifications: Manufacturer: JBO Tool Type: GF SHARK THREADMILL
ISCAR
Associated Technologies and Manufacturing Inc., a 25-man Baton Rouge contract fabrication shop specializing in silicon and energy oil country components, found plunge milling to be the answer to its production problems. ATM wished to speed up production and cut high tooling costs when endmilling long pockets in a steel prone to work hardening. The company switched from a solid cobalt end mill to a two-flute Punch- In Quad DHU Series indexable plunge mill from Ingersoll Cutting Tools. “With that one simple processing change, we’ve made work hardening a thing of the past, saving us 10 hours of machining time and $880 in tooling per part,” said Glen Kollars, lead machinist at ATM. “Now we complete a 44-in.-long square-sided pocket with a single tool instead of three. The plunge mill paid for itself on the very first part.”
Kollars loaded the DHU and, following DeLucca’s and Dees’s recommendations, modified the program in ATM’s G81 software. “It worked like a charm beginning with the first part,” Kollars said. “Machining time for the pair of slots dropped from 40 to 30 hours, all touch-up machining was eliminated and the insert edges looked as good as new after finishing both slots. And we’re completing the slots with the single tool and single setup.” On that basis, ATM projects a significant dollar saving per part.
Plunge milling vs drilling
Eliminating deflection The part is an 8.375-in.-diameter by 100-in.- long shaft of wrought 4140 HT steel with two opposing pockets running lengthwise. The pockets will contain instrumentation that must fit within the shaft diameter. Measuring 44-in. long with a 4.750 by 3.625-in. cross section, the pockets have straight sides, flat bottoms and reliefs in the corners to accommodate a tightfitting sharp-cornered cover. After machining, a 1.125-in. web separates the two pockets.
End millplungingspeeds
However, the first plunge cutter that Kollars tried didn’t work out because its insert geometry didn’t include back relief. As a result, the tool rubbed the pocket wall upon withdrawal, causing some deflection, premature edge wear and enough cutting friction to work harden the material.
With end mills that might snap at anytime, Kollars always had to keep an eye on the operation. “This also suits the working style of our shop, where our machinists can set their own work schedule as long as we put in our total hours. We’re not tied to the workplace just because a long-cycle pocket-milling operation is being machined."
Seco plunge milling cutters
Plunging payoff Ingersoll’s Derek Delucca and Kevin Dees established cutting parameters. Since ATM’s vertical machining center lacked through-spindle coolant capability for chip evacuation, they recommended running the cutter at 1,735 rpm, 17 ipm, with a surprisingly small 0.050- to 0.060-in. stepover and air blast for chip removal.
ATM’s Glen Kollars (center) confers with Ingersoll’s Kevin Dees (left) and MDM’s Joe Cazedessus on plunge-milling cutting strategy. Previously it took about 40 hours and three different end mills to complete the two pockets on a 40-taper Mighty-Comet machining center. “But speed wasn’t the main problem,” Kollars explained. “Rather it was the variations in pocket width and wall straightness due to tool deflection. We had to do a lot of touch-up machining to make the covers fit right. Also, due to that deflection, once the edges began to dull, cutters would snap off at the rate of about eight per part on average.” Mainly to overcome the tool breakage, Kollars decided to try plunge milling for the hogging, followed by end milling to straighten the walls and put in the square corner around the bottom. “In theory, plunge milling should work because all the cutting forces are axial,” he said. However, the first plunge cutter that Kollars tried didn’t work out because its insert geometry didn’t include back relief. As a result, the tool rubbed the pocket wall upon withdrawal, causing some deflection, premature edge wear and enough cutting friction to work harden the material. Then he asked his distributor, Joe Cazedessus of MDM Total Supply in Baton Rouge to recommend a true plunge cutter. Cazedessus suggested he check out the plunge cutter section of the Ingersoll e-catalog, and after careful study, Kollars settled on a 0.75-in. Ingersoll 750 DHU plunge mill. “The inserts were square and had the correct back relief to ensure a 100% plunge cutting action. This was a true plunge cutter.” The Ingersoll DHU plunge cutter features positive-positive geometry for on-track cutting and square inserts with back relief to avoid rubbing sidewalls behind the cutting face. The 0.75- in.-diameter end mill head is equipped with the Top On modular adaptation that connects with various steel and carbide toolholders. It is also designed for through-the-tool coolant delivery. Plunging payoff Ingersoll’s Derek Delucca and Kevin Dees established cutting parameters. Since ATM’s vertical machining center lacked through-spindle coolant capability for chip evacuation, they recommended running the cutter at 1,735 rpm, 17 ipm, with a surprisingly small 0.050- to 0.060-in. stepover and air blast for chip removal. “While the small stepover would slow the hogging removal rate a little,” said DeLucca, “the resulting scalloped peaks would be small enough to meet tolerances without subsequent operations and attendant tool changes.” At 0.060-in. stepover, a 0.75-in. cutter leaves scallop ridges just 0.002-in. high, well within tolerances for the part. Kollars loaded the DHU and, following DeLucca’s and Dees’s recommendations, modified the program in ATM’s G81 software. “It worked like a charm beginning with the first part,” Kollars said. “Machining time for the pair of slots dropped from 40 to 30 hours, all touch-up machining was eliminated and the insert edges looked as good as new after finishing both slots. And we’re completing the slots with the single tool and single setup.” On that basis, ATM projects a significant dollar saving per part. ATM starts the slot by plunging to full depth into solid metal, being careful to blast out the chips. This is at the site of a through hole that later will join the opposing slots. There is a 0.75-in. through hole at either end of the slots. Ever since the startup, ATM has stuck with those original settings. As a precaution, they change inserts after every two slots. “That’s about $20 worth of inserts versus eight solidcarbide endmills at $110 a pop, plus the two additional finishing endmills,” Kollars said. “Now the only tooling inventory we need for the entire slotting operation is a little packet of inserts and nothing more.” Building on success Based on that success, ATM has standardized on the Ingersoll DHU plunge mill for all slotting and pocket milling, with nearly the same margins of improvement. “We’ve also had great success on thin-wall stock,” added Kollars. “Because the cutting is purely axial, the cutter tracks true, without any side forces that might distort a fragile workpiece.” On one thinwall part, ATM plunges out a pocket at 1,700 rpm and 10 ipm without any part distortion. A job that once took an hour is done in 20 to 30 minutes. Kollars also likes the added process security of plunge milling. ATM can run the operation unattended, even “lights out” as long as there’s a reliable chip-disposal system in place. With end mills that might snap at anytime, Kollars always had to keep an eye on the operation. “This also suits the working style of our shop, where our machinists can set their own work schedule as long as we put in our total hours. We’re not tied to the workplace just because a long-cycle pocket-milling operation is being machined."
It features exposed carbon-fiber bodywork over a Dark Energy Alcantara interior, and it was also optioned with six-point harness anchors, a leather-wrapped ...
Specially designed for 2D and 3D CNC profiling and carving in plastic, aluminum & wood with CNC machines. The high-shear ball nose tips cut smooth 2D and 3D ...
Then he asked his distributor, Joe Cazedessus of MDM Total Supply in Baton Rouge to recommend a true plunge cutter. Cazedessus suggested he check out the plunge cutter section of the Ingersoll e-catalog, and after careful study, Kollars settled on a 0.75-in. Ingersoll 750 DHU plunge mill. “The inserts were square and had the correct back relief to ensure a 100% plunge cutting action. This was a true plunge cutter.”
Plunge end mill
Thread milling is also a machining process. The thread milling cutter can mill an internal and external thread and can also be used on thin-walled workpieces.
Plunge milling works much like drilling: plunge straight in, withdraw, step over plunge again, and so on. Since all the cutting force vectors are right up the tool’s strong centerline, you can safely feed faster by plunging along the Z axis than by end-milling along the X and Y axes. Plunging leaves a scalloped wall that may require finish milling, depending on tolerances and size of the stepover. Plunge cutters also have built-in chip evacuation capacity, so blast air or liquid coolant is helpful but not required on vertical setups.
Undercutting is needed to restore the desired ballast properties after becoming fouled. Undercutting is the continuous excavation of the material beneath the ...
Previously it took about 40 hours and three different end mills to complete the two pockets on a 40-taper Mighty-Comet machining center. “But speed wasn’t the main problem,” Kollars explained. “Rather it was the variations in pocket width and wall straightness due to tool deflection. We had to do a lot of touch-up machining to make the covers fit right. Also, due to that deflection, once the edges began to dull, cutters would snap off at the rate of about eight per part on average.”
ATM starts the slot by plunging to full depth into solid metal, being careful to blast out the chips. This is at the site of a through hole that later will join the opposing slots. There is a 0.75-in. through hole at either end of the slots.
Plunge milling feeds and speeds
Mainly to overcome the tool breakage, Kollars decided to try plunge milling for the hogging, followed by end milling to straighten the walls and put in the square corner around the bottom. “In theory, plunge milling should work because all the cutting forces are axial,” he said.
The chemical element nickel is classed as a transition metal. In the 1750s nickel was discovered to be an element by Axel Cronstedt.
Karnasch has developed an individual range of tools for any challenges of graphite machining. In addition to solid carbide end mills, solid carbide drills, ...
Best end mill forplunging
Building on success Based on that success, ATM has standardized on the Ingersoll DHU plunge mill for all slotting and pocket milling, with nearly the same margins of improvement. “We’ve also had great success on thin-wall stock,” added Kollars. “Because the cutting is purely axial, the cutter tracks true, without any side forces that might distort a fragile workpiece.” On one thinwall part, ATM plunges out a pocket at 1,700 rpm and 10 ipm without any part distortion. A job that once took an hour is done in 20 to 30 minutes.
When end milling long pockets, cutting forces can cause deflections along the tool’s X and Y axes resulting in workpiece dimensional variations. These forces can lead to tool breakage. On the other hand, with plunge milling, the cutting force vector runs straight up the tool centerline, so you can cut with more force without fear of bending or snapping the tool.
The Ingersoll DHU plunge cutter features positive-positive geometry for on-track cutting and square inserts with back relief to avoid rubbing sidewalls behind the cutting face. The 0.75- in.-diameter end mill head is equipped with the Top On modular adaptation that connects with various steel and carbide toolholders. It is also designed for through-the-tool coolant delivery.
Ever since the startup, ATM has stuck with those original settings. As a precaution, they change inserts after every two slots. “That’s about $20 worth of inserts versus eight solidcarbide endmills at $110 a pop, plus the two additional finishing endmills,” Kollars said. “Now the only tooling inventory we need for the entire slotting operation is a little packet of inserts and nothing more.”
Titan Vinyl Cutters · USCutter TITAN 3 ARMS Contour Cutting Vinyl Cutter - 28" | 53" | 68 · USCutter 28" / 53" TITAN 2 Vinyl Cutter w/ VinylMaster Cut Software.
202325 — 5. The loads on the teeth are acting gradually. Non Conventional Milling 1. This machine poses a longer tool life. 2. This machine produces a ...
Kollars also likes the added process security of plunge milling. ATM can run the operation unattended, even “lights out” as long as there’s a reliable chip-disposal system in place.
2024915 — From the aesthetic point of view, spot facing may be preferable. You need to drill very precisely on a curved surface to avoid skidding off from ...
If you have difficulty reading the text in the PDF viewer, please click the button to view the PDF in full-screen mode, or enlarge the text by clicking on the appropriate area. You can also download the PDF file from the viewer.
 18581906093