
BALL NOSE CUTTERS - INDEXABLE - MILLING - insert milling ball finish
1999121 — First, use only a high quality tungsten carbide to machine graphite. Yes high-speed steel could be used, but tool life is limited. The tool ...
As with meteorology and pharmacology, however, the interrelationship of theory and practice has been developing over decades as the theory part of the balance becomes more advanced thanks to information technology. For example, an effort called the Machine Tool Genome Project is working toward providing the computer modeling (simulation) needed to predict optimal speed-and-feed combinations for particular setups in any internet-connected shop with less local experimentation and testing.[15] Instead of the only option being the measuring and testing of the behavior of its own equipment, it will benefit from others' experience and simulation; in a sense, rather than 'reinventing a wheel', it will be able to 'make better use of existing wheels already developed by others in remote locations'.
For a given machining operation, the cutting speed will remain constant for most situations; therefore the spindle speed will also remain constant. However, facing, forming, parting off, and recess operations on a lathe or screw machine involve the machining of a constantly changing diameter. Ideally, this means changing the spindle speed as the cut advances across the face of the workpiece, producing constant surface speed (CSS). Mechanical arrangements to effect CSS have existed for centuries, but they were never applied commonly to machine tool control. In the pre-CNC era, the ideal of CSS was ignored for most work. For unusual work that demanded it, special pains were taken to achieve it. The introduction of CNC-controlled lathes has provided a practical, everyday solution via automated CSS Machining Process Monitoring and Control. By means of the machine's software and variable speed electric motors, the lathe can increase the RPM of the spindle as the cutter gets closer to the center of the part.
We offer high-quality solid carbide end mills and tools like ball nose endmills, carbide drills, and end mill cutters that our valued customers trust and ...
Generally speaking, spindle speeds and feed rates are less critical in woodworking than metalworking. Most woodworking machines including power saws such as circular saws and band saws, jointers, Thickness planers rotate at a fixed RPM. In those machines, cutting speed is regulated through the feed rate. The required feed rate can be extremely variable depending on the power of the motor, the hardness of the wood or other material being machined, and the sharpness of the cutting tool.
SFM to RPM
Our Peeling Inserts are meticulously engineered to provide exceptional cutting efficiency and precision.Whether you require inserts for roughing, finishing, ...
LATHE CARBIDE INSERT HOLDER,carbide insert quotation, drilling inserts suppliers, grooving inserts manufacturers, milling inserts factory, Contact us for an ...
e.g. for a cutting speed of 100 ft/min (a plain HSS steel cutter on mild steel) and diameter of 10 inches (the cutter or the work piece)
The machinability rating of a material attempts to quantify the machinability of various materials. It is expressed as a percentage or a normalized value. The American Iron and Steel Institute (AISI) determined machinability ratings for a wide variety of materials by running turning tests at 180 surface feet per minute (sfpm). It then arbitrarily assigned 160 Brinell B1112 steel a machinability rating of 100%. The machinability rating is determined by measuring the weighed averages of the normal cutting speed, surface finish, and tool life for each material. Note that a material with a machinability rating less than 100% would be more difficult to machine than B1112 and material and a value more than 100% would be easier.
Neo-Grotesque typefaces include some of the most common typefaces: MS Sans Serif, Arial, Helvetica and Univers are all neo-grotesque sans serif type fonts. They have a relatively plain appearance when compared to the grotesques.
Speed-and-feed selection is analogous to other examples of applied science, such as meteorology or pharmacology, in that the theoretical modeling is necessary and useful but can never fully predict the reality of specific cases because of the massively multivariate environment. Just as weather forecasts or drug dosages can be modeled with fair accuracy, but never with complete certainty, machinists can predict with charts and formulas the approximate speed and feed values that will work best on a particular job, but cannot know the exact optimal values until running the job. In CNC machining, usually the programmer programs speeds and feedrates that are as maximally tuned as calculations and general guidelines can supply. The operator then fine-tunes the values while running the machine, based on sights, sounds, smells, temperatures, tolerance holding, and tool tip lifespan. Under proper management, the revised values are captured for future use, so that when a program is run again later, this work need not be duplicated.
Tails are sometimes-decorative descending strokes, as seen on an uppercase “R”. Finials are the tapered endings of some strokes. Shoulders are any curved stroke that originate from a stem.
Crossbars are horizontal strokes, as found on the uppercase “A” and “H”. Terminals are only found on serif characters, and are the end of any line that doesn’t have a serif. Loops are found on some lowercase “g” characters, and can be fully closed or partially closed.
Thanks for taking the time to type this up and publish it. This is a PERFECT crash course for typeface. Gives you everything you need to know if you just want the basics, and is a great jumping point for anyone who wants to know more. Well done.
Grinding wheels are designed to be run at a maximum safe speed, the spindle speed of the grinding machine may be variable but this should only be changed with due attention to the safe working speed of the wheel. As a wheel wears it will decrease in diameter, and its effective cutting speed will be reduced. Some grinders have the provision to increase the spindle speed, which corrects for this loss of cutting ability; however, increasing the speed beyond the wheels rating will destroy the wheel and create a serious hazard to life and limb.
Modern serifs, which include typefaces like Didot and Bodoni, have a much more pronounced contrast between thin and thick lines, and have have a vertical stress and minimal brackets. They date back to the late 1700s.
CY Carbide manufactures different types of carbide milling inserts: General Milling Inserts, High Hardness Milling Inserts, and High Feed Inserts.
The exact RPM is not always needed, a close approximation will work. For instance, a machinist may want to take the value of π {\displaystyle {\pi }} to be 3 if performing calculations by hand.
Scientific study by Holz and De Leeuw of the Cincinnati Milling Machine Company[17] did for milling cutters what F. W. Taylor had done for single-point cutters.
Spurs are tiny projections from curved strokes, such as on some uppercase “G” characters. Links connect the top and bottom bowls of a double-stacked lowercase “g”. The spine is the curved stroke found on the letter “s”.
The final main type of serif typeface is the slab serif. Slab serifs have little to no contrast between thick and thin lines, and have thick, rectangular serifs, and sometimes have fixed widths. The underlying characters hapes often more closely resemble sans serif fonts.
When calculating for copper alloys, the machine rating is arrived at by assuming the 100 rating of 600 SFM. For example, phosphorus bronze (grades A–D) has a machinability rating of 20. This means that phosphor bronze runs at 20% the speed of 600 SFM or 120 SFM. However, 165 SFM is generally accepted as the basic 100% rating for "grading steels".[12] Formula Cutting Speed (V)= [πDN]/1000 m/min Where D=Diameter of Workpiece in meter or millimeter N=Spindle Speed in rpm
When most of us talk about “fonts”, we’re really talking about typefaces, or type families (which are groups of typefaces with related designs).
"Following World War II, many new alloys were developed. New standards were needed to increase [U.S.] American productivity. Metcut Research Associates, with technical support from the Air Force Materials Laboratory and the Army Science and Technology Laboratory, published the first Machining Data Handbook in 1966. The recommended speeds and feeds provided in this book were the result of extensive testing to determine optimum tool life under controlled conditions for every material of the day, operation and hardness."[4]
Machinability ratings can be used in conjunction with the Taylor tool life equation, VTn = C in order to determine cutting speeds or tool life. It is known that B1112 has a tool life of 60 minutes at a cutting speed of 100 sfpm. If a material has a machinability rating of 70%, it can be determined, with the above knowns, that in order to maintain the same tool life (60 minutes), the cutting speed must be 70 sfpm (assuming the same tooling is used).
very interested in the debate around the readability of serif type online. Where does this come from? It goes against everything I ever learned after years in the graphic arts and publishing business.
The aperture of a character refers to the opening at the bottom of some characters, such as the uppercase “A” or lowercase “m”. An ear is a decorative extension on a letter, as highlighted on the “g” above. Hairlines are the thinnest part of a serif typeface.
The different letterforms within a typeface share a few common characteristics. These characteristics can be important in determining whether two (or more) typefaces work well together, or clash. Here are the most basic parts of a typeface:
In this part, we’ll talk about the basics of typographic theory, including the different kinds of typefaces (and how typefaces and fonts differ), as well as the basic anatomy of a typeface. And each part will also offer more resources for delving deeper into typography.
Feed rate is the velocity at which the cutter is fed, that is, advanced against the workpiece. It is expressed in units of distance per revolution for turning and boring (typically inches per revolution [ipr] or millimeters per revolution). It can be expressed thus for milling also, but it is often expressed in units of distance per time for milling (typically inches per minute [ipm] or millimeters per minute), with considerations of how many teeth (or flutes) the cutter has then determined what that means for each tooth.
Great examples, but if you're going to each a lesson on typography, you should realize the AWFUL GAPING HOLES in the kerning of said examples!! Specifically, the 2nd graphic "Crimson text is a serif typeface" .. I found that via google search about typography examples and was a tad shocked.
Thank you. My wife was a graphic designer when I met her. Later a creative director in the world of print advertising. When we first started dating she said that for me to fully understand what she does and what she values I would have to learn about type. I spend our first few dates learning and setting type. We looked at type books and she taught me how to use a Schaedlere ruler. I came to love the dedication and belief she had in the art of type and what it could do on a printed page. Type spoke as much as the language. How could you not fall in love with someone like her who would move a period a 16th of an inch to make the headline work better. I miss her.
BENCHMARK FOR SPEED AND FEED ; ø Cutting Speed m/min.*. End Mill Diamater ; ø Cutting Speed m/min.* · ø 1 mm. ø 2 mm. ø 3 mm.
Sans-serif typefaces are called such because they lack serif details on characters. Sans-serif typefaces are often more modern in appearance than serifs. The first sans-serifs were created in the late 18th century.
Wow, this is probably the best typography explanation for a design beginner like myself. You made it super easy to understand. Thank you!
Most metalworking books have nomograms or tables of spindle speeds and feed rates for different cutters and workpiece materials; similar tables are also likely available from the manufacturer of the cutter used.
Cutting speed and feed rate come together with depth of cut to determine the material removal rate, which is the volume of workpiece material (metal, wood, plastic, etc.) that can be removed per time unit.
Spindle speed becomes important in the operation of routers, spindle moulders or shapers, and drills. Older and smaller routers often rotate at a fixed spindle speed, usually between 20,000 and 25,000 rpm. While these speeds are fine for small router bits, using larger bits, say more than 1-inch (25 mm) or 25 millimeters in diameter, can be dangerous and can lead to chatter. Larger routers now have variable speeds and larger bits require slower speed. Drilling wood generally uses higher spindle speeds than metal, and the speed is not as critical. However, larger diameter drill bits do require slower speeds to avoid burning.
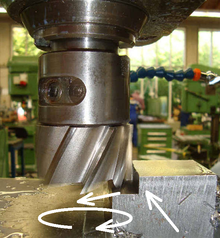
Cutting speed may be defined as the rate at the workpiece surface, irrespective of the machining operation used. A cutting speed for mild steel of 100 ft/min is the same whether it is the speed of the cutter passing over the workpiece, such as in a turning operation, or the speed of the cutter moving past a workpiece, such as in a milling operation. The cutting conditions will affect the value of this surface speed for mild steel.
There will be an optimum cutting speed for each material and set of machining conditions, and the spindle speed (RPM) can be calculated from this speed. Factors affecting the calculation of cutting speed are:
There are three general styles you’ll find with many typefaces: italic, oblique, and small caps. Small caps are often used for headings or subheadings, to add variety to your typography if using a single typeface.
Some typefaces are more transcendent, and can convey almost any mood based on the content and the other typefaces they’re combined with. Helvetica is often considered one such font.
The spindle speeds may be calculated for all machining operations once the SFM or MPM is known. In most cases, we are dealing with a cylindrical object such as a milling cutter or a workpiece turning in a lathe so we need to determine the speed at the periphery of this round object. This speed at the periphery (of a point on the circumference, moving past a stationary point) will depend on the rotational speed (RPM) and diameter of the object.
Cutting speed (also called surface speed or simply speed) is the speed difference (relative velocity) between the cutting tool and the surface of the workpiece it is operating on. It is expressed in units of distance across the workpiece surface per unit of time, typically surface feet per minute (sfm) or meters per minute (m/min).[1] Feed rate (also often styled as a solid compound, feedrate, or called simply feed) is the relative velocity at which the cutter is advanced along the workpiece; its vector is perpendicular to the vector of cutting speed. Feed rate units depend on the motion of the tool and workpiece; when the workpiece rotates (e.g., in turning and boring), the units are almost always distance per spindle revolution (inches per revolution [in/rev or ipr] or millimeters per revolution [mm/rev]).[2] When the workpiece does not rotate (e.g., in milling), the units are typically distance per time (inches per minute [in/min or ipm] or millimeters per minute [mm/min]), although distance per revolution or per cutter tooth are also sometimes used.[2]
This series aims to change that. If you’re intimidated by typography, or even just aren’t quite sure where to start, then read on. We’ll break down typographic theory and practice, starting with the basics (so that everyone starts on the same page).
The phrase speeds and feeds or feeds and speeds refers to two separate parameters in machine tool practice, cutting speed and feed rate. They are often considered as a pair because of their combined effect on the cutting process. Each, however, can also be considered and analyzed in its own right.
The cutting speed is given as a set of constants that are available from the material manufacturer or supplier. The most common materials are available in reference books or charts, but will always be subject to adjustment depending on the cutting conditions. The following table gives the cutting speeds for a selection of common materials under one set of conditions. The conditions are a tool life of 1 hour, dry cutting (no coolant), and at medium feeds, so they may appear to be incorrect depending on circumstances. These cutting speeds may change if, for instance, adequate coolant is available or an improved grade of HSS is used (such as one that includes [cobalt]).
Dingbats are specialty typefaces that consist of symbols and ornaments instead of letters. Wingdings is probably the best-known dingbat font, though there are now thousands, often created around themes.
Old Style serifs (also called humanist) are the oldest typefaces in this classification, dating back to the mid 1400s. The main characteristic of old style characters is their diagonal stress (the thinnest parts of the letters appear on the angled strokes, rather than the vertical or horizontal ones). Typefaces in this category include Adobe Jenson, Centaur, and Goudy Old Style.
Italic and oblique are often confused or used interchangeably, but are two distinct styles. Oblique type is simply a slanted version of the regular characters. You could create this using the “distort” function in Photoshop, although sometimes a separate oblique font is included within a typeface. Italics are slanted like obliques, but are actually a separate set of characters, with their own unique letterforms.
201213 — Most hacksaws come equipped with a 24 TPI (teeth per inch) blade that will work for most jobs, including cutting a carbon fiber bar or steerer ...
Schematically, speed at the workpiece surface can be thought of as the tangential speed at the tool-cutter interface, that is, how fast the material moves past the cutting edge of the tool, although "which surface to focus on" is a topic with several valid answers. In drilling and milling, the outside diameter of the tool is the widely agreed surface. In turning and boring, the surface can be defined on either side of the depth of cut, that is, either the starting surface or the ending surface, with neither definition being "wrong" as long as the people involved understand the difference. An experienced machinist summed this up succinctly as "the diameter I am turning from" versus "the diameter I am turning to."[4] He uses the "from", not the "to", and explains why, while acknowledging that some others do not. The logic of focusing on the largest diameter involved (OD of drill or end mill, starting diameter of turned workpiece) is that this is where the highest tangential speed is, with the most heat generation, which is the main driver of tool wear.[4]
When deciding what feed rate to use for a certain cutting operation, the calculation is fairly straightforward for single-point cutting tools, because all of the cutting work is done at one point (done by "one tooth", as it were). With a milling machine or jointer, where multi-tipped/multi-fluted cutting tools are involved, then the desired feed rate becomes dependent on the number of teeth on the cutter, as well as the desired amount of material per tooth to cut (expressed as chip load). The greater the number of cutting edges, the higher the feed rate permissible: for a cutting edge to work efficiently it must remove sufficient material to cut rather than rub; it also must do its fair share of work.
Grotesques are the earliest, and include fonts like Franklin Gothic and Akzidenz Grotesk. These typefaces often have letterforms that are very similar to serif typefaces, minus the serifs.
Also included among display typefaces are blackletter typefaces, which were the original typefaces used with the first printing presses. Since that time, better, more readable fonts have been developed.
The above image shows the different guidelines that are generally present in a typeface. The baseline is the invisible line that all the characters sit on. Rounded letters sometimes sit just a tiny bit under the baseline, and descenders always drop below this line. A given typeface will have a consistent baseline.
Scripts are based upon handwriting, and offer very fluid letterforms. There are two basic classifications: formal and casual. Formal scripts are often reminiscent of the handwritten letterforms common in the 17th and 18th centuries. Some scripts are based directly on the handwriting of masters like George Snell and George Bickham. There are modern creations, too, including Kuenstler Script. They’re common for very elegant and elevated typographical designs, and are unsuitable for body copy.
Outside of the context of machine tooling, "speeds and feeds" can be used colloquially to refer to the technical details of a product or process.[3]
The spindle speed is the rotational frequency of the spindle of the machine, measured in revolutions per minute (RPM). The preferred speed is determined by working backward from the desired surface speed (sfm or m/min) and incorporating the diameter (of workpiece or cutter).
One analogy would be a skateboard rider and a bicycle rider travelling side by side along the road. For a given surface speed (the speed of this pair along the road) the rotational speed (RPM) of their wheels (large for the skater and small for the bicycle rider) will be different. This rotational speed (RPM) is what we are calculating, given a fixed surface speed (speed along the road) and known values for their wheel sizes (cutter or workpiece).
A lot of people use the terms “typeface” and “font” interchangeably. But they’re two very distinct things. Before we get started talking about typography, let’s get our terms straight.
A typeface is a set of typographical symbols and characters. It’s the letters, numbers, and other characters that let us put words on paper (or screen). A font, on the other hand, is traditionally defined as a complete character set within a typeface, often of a particular size and style. Fonts are also specific computer files that contain all the characters and glyphs within a typeface.
Geometric sans-serifs are more closely based on geometric shapes. Generally, the “O”s in geometrics will appear circular, and the letter “a” is almost always simple, just a circle with a tail. They’re the least commonly-used for body copy, and are also the most modern sans-serifs, as a general rule.
Cutting feeds and speeds, and the spindle speeds that are derived from them, are the ideal cutting conditions for a tool. If the conditions are less than ideal then adjustments are made to the spindle's speed, this adjustment is usually a reduction in RPM to the closest available speed, or one that is deemed (through knowledge and experience) to be correct.
In woodworking, the ideal feed rate is one that is slow enough not to bog down the motor, yet fast enough to avoid burning the material. Certain woods, such as black cherry and maple are more prone to burning than others. The right feed rate is usually obtained by "feel" if the material is hand fed, or by trial and error if a power feeder is used. In thicknessers (planers), the wood is usually fed automatically through rubber or corrugated steel rollers. Some of these machines allow varying the feed rate, usually by changing pulleys. A slower feed rate usually results in a finer surface as more cuts are made for any length of wood.
There are a number of different ways to classify typefaces and type families. The most common classifications are by technical style: serif, sans-serif, script, display, and so on. Typefaces are also classified by other technical specifications, such as proportional vs. monospaced, or by more fluid and interpretational definitions, such as the mood they create.
Typography could be considered the most important part of any design. It’s definitely among the most important elements of any design project. And yet it’s often the part of a design that’s left for last, or barely considered at all. Designers are often intimidated by typography, which can result in bland typographical design or a designer always using one or two “reliable” typefaces in their designs.
The meanline is the height of most of the lowercase characters within a typeface, and is generally based on the lowercase “x” if there are varying heights among the lowercase characters. This is also where the term “x-height” comes from. The cap height is the distance between the baseline and the top of uppercase letters like “A”.
Serif typefaces are called “serifs” in reference to the small lines that are attached to the main strokes of characters within the face. Serif typefaces are most often used for body copy in print documents, as well as for both body text and headlines online. The readability of serifs online has been debated, and some designers prefer not to use serifs for large blocks of copy.
The ratio of the spindle speed and the feed rate controls how aggressive the cut is, and the nature of the swarf formed.
Speeds and feeds have been studied scientifically since at least the 1890s. The work is typically done in engineering laboratories, with the funding coming from three basic roots: corporations, governments (including their militaries), and universities. All three types of institution have invested large amounts of money in the cause, often in collaborative partnerships. Examples of such work are highlighted below.
The mood of a typeface is an important part of how it should be used. Different typefaces have strikingly different moods. Commonly used moods include formal vs. informal, modern vs classic/traditional, and light vs dramatic. Some typefaces have very distinct moods. For example, Times New Roman is pretty much always going to be a traditional font, which is why it’s so commonly used for business correspondence. Verdana, on the other hand, has a more modern mood.
This formula[14] can be used to figure out the feed rate that the cutter travels into or around the work. This would apply to cutters on a milling machine, drill press and a number of other machine tools. This is not to be used on the lathe for turning operations, as the feed rate on a lathe is given as feed per revolution.
Humanist typefaces include Gill Sans, Frutiger, Tahoma, Verdana, Optima, and Lucide Grande. These are more calligraphic than other sans-serif typefaces, and are also the most legible (hence the popularity of some of them for website body copy). They’re more calligraphic than other sans-serifs, meaning they have a greater variation in line widths.
The ascender of a lowercase character is any part that rises above the meanline, such as the uprights on the letters “d”, “h”, and “b”. Descenders are the parts of a lowercase character that drop below the baseline, such as in a “p”, “q” or “g”.
Serifs are the extra flourish at the end of a stroke on serif typefaces. Some typefaces have very pronounced serifs, while others are barely distinguishable.
This is exactly what I was looking for. As a beginner like myself, this article helps to clear confusion regarding different technical terms ( geometric, Grotesque, Humanist... etc. ) used to describe a typeface.
Milling Cutter ; Low Resistance Tangential Insert Slotting Cutter. Seri TGC ; High-efficiency and High-rigidity Radius Milling Cutter. SEC-Wave Radius Mill. Seri ...
The above illustration shows three common parts to letterforms. The stem is the main upright of any letter, including the primary diagonal. It’s could be considered the anchor of the character. The bar is any horizontal part, which are sometimes also called arms. The bowl is the curved part of a character that creates an interior empty space. The inside of a bowl is a counter.
Next Monday we’ll discuss paragraph composition and using special typographic characters, like ligatures and hyphens. We’ll dive right into basic typographic layouts, and how to decide on a typeface for your project. Stay tuned!
To all those whom have disgraced my article "A Crash Course in Typography", I have seen all of your crude comments such as "penis", or "bottom text", as well as the spam comments. I am looking into creating a character limit on these comments, as well as a requirement to confirm that your email is in fact yours. I find all of this very childish, and I am really bothered by it. I'd appreciate you all resisting the urge to do these things to other peoples possessions. Sincerely- Chapman
If variables such as cutter geometry and the rigidity of the machine tool and its tooling setup could be ideally maximized (and reduced to negligible constants), then only a lack of power (that is, kilowatts or horsepower) available to the spindle would prevent the use of the maximum possible speeds and feeds for any given workpiece material and cutter material. Of course, in reality those other variables are dynamic and not negligible, but there is still a correlation between power available and feeds and speeds employed. In practice, lack of rigidity is usually the limiting constraint.
A study on the effect of the variation of cutting parameters in the surface integrity in turning of an AISI 304 stainless steel revealed that the feed rate has the greatest impairing effect on the quality of the surface, and that besides the achievement of the desired roughness profile, it is necessary to analyze the effect of speed and feed on the creation of micropits and microdefects on the machined surface.[18] Moreover, they found that the conventional empirical relation that relates feed rate to roughness value does not fit adequately for low cutting speeds.
We will go over 6 different typefaces which are own characters. You can find a diverse range of fonts under these typefaces.
Casual scripts more closely resemble modern handwriting, and date back to the mid-twentieth century. They’re much less formal, often with stronger strokes and a more brush-like appearance. Casual scripts include Mistral and Brush Script.
Some materials, such as machinable wax, can be cut at a wide variety of spindle speeds, while others, such as stainless steel require much more careful control as the cutting speed is critical, to avoid overheating both the cutter and workpiece. Stainless steel is one material that hardens very easily under cold working, therefore insufficient feed rate or incorrect spindle speed can lead to less than ideal cutting conditions as the work piece will quickly harden and resist the tool's cutting action. The liberal application of cutting fluid can improve these cutting conditions; however, the correct selection of speeds is the critical factor.
Display typefaces are probably the broadest category and include the most variation. The main characteristic is that they’re unsuitable for body copy and are best reserved for headlines or other short copy that needs attention drawn to it. Display typefaces can be formal, or informal, and evoke any kind of mood. They’re more commonly seen in print design, but are becoming more popular online with the use of web fonts.
Excessive spindle speed will cause premature tool wear, breakages, and can cause tool chatter, all of which can lead to potentially dangerous conditions. Using the correct spindle speed for the material and tools will greatly enhance tool life and the quality of the surface finish.
Thank you for this. Just starting out on my journey into design and this was very simple and easy to follow and to understand. Thank you for writing it :)
In the 1890s through 1910s, Frederick Winslow Taylor performed turning experiments[16] that became famous (and seminal). He developed Taylor's Equation for Tool Life Expectancy.
Tapping speed
Within the majority of typefaces, you’ll find more than one style and/or weight. Weights are often classified as “light”, “thin”, “regular”, “medium”, “bold”, “heavy”, or “black”. Each of these refers to the thickness of the strokes that make up the characters:
In proportional typefaces, the space a character takes up is dependent on the natural width of that character. An “i” takes up less space than an “m”, for example. Times New Roman is a proportional typeface. In monospace typefaces, on the other hand, each character takes up the same amount of space. Narrower characters simply get a bit more spacing around them to make up for the difference in width. Courier New is one example of a monospace typeface.
201785 — Hardness is the ability of the material to resist the scratch and indentation on metal surface. Unit-normally Kgf/cm2. Brinnel Hardness(BHN), ...
202374 — Cutting aluminum sheet requires the right tools, technique and safety awareness. Hand cutting and power tool cutting are commonly used methods.
Transitional serifs date back to the mid 1700s, and are generally the most common serif typefaces. Times New Roman and Baskerville are both transitional serif fonts, as are Caslon, Georgia, and Bookman. The differences between thick and thin strokes in transitional typefaces are more pronounced than they are in old style serifs, but less so than in modern serifs.
Thank you for the interesting article. For a beginning enthusiast in typesetting like me, this article is a great introduction to the field. Looking forward to going through the entire course.



 18581906093